



The Problem: Cycle Time Is the Silent Margin Killer
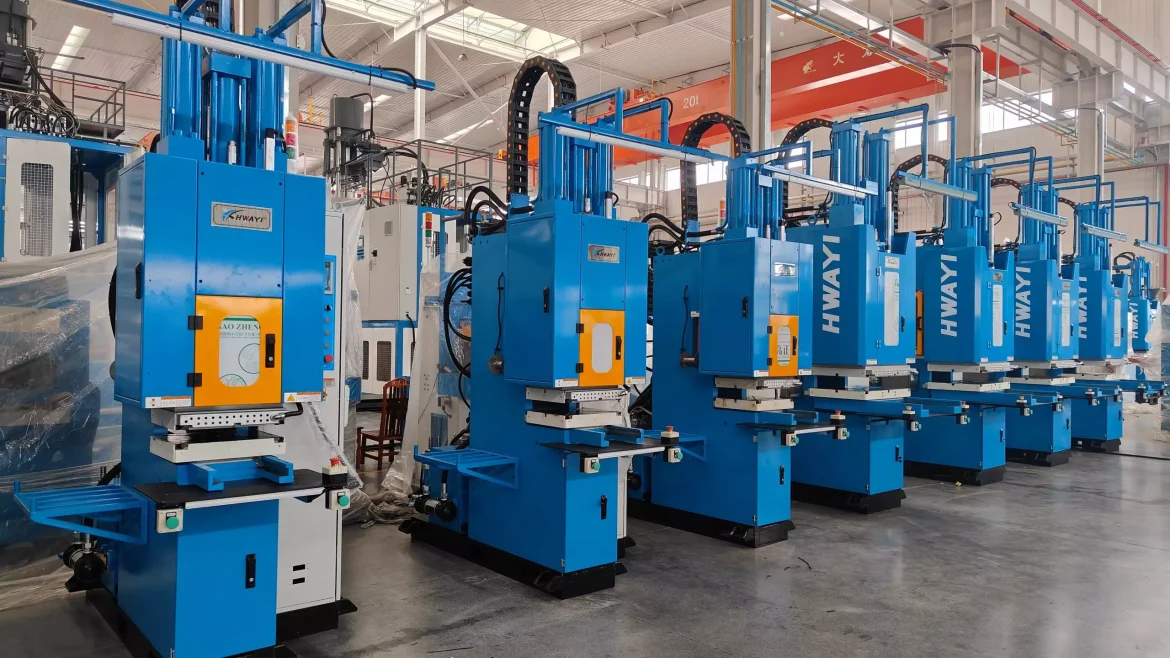
Production lines grind when demolding stalls. For rubber shops that run high-volume runs, unpredictable mold release and long cure time drag takt down and eat margin. The typical fixes—faster press speeds or larger shot sizes—often swap one bottleneck for another. What actually moves the needle is hardware designed for consistent demolding and automatic strip workflows, like those found on modern rubber injection molding machine platforms. Industry players from small gasket shops to automotive suppliers in Japan have leaned on these systems to stabilize takt and hit delivery windows during recent supply shocks.
Root Causes Broken Down
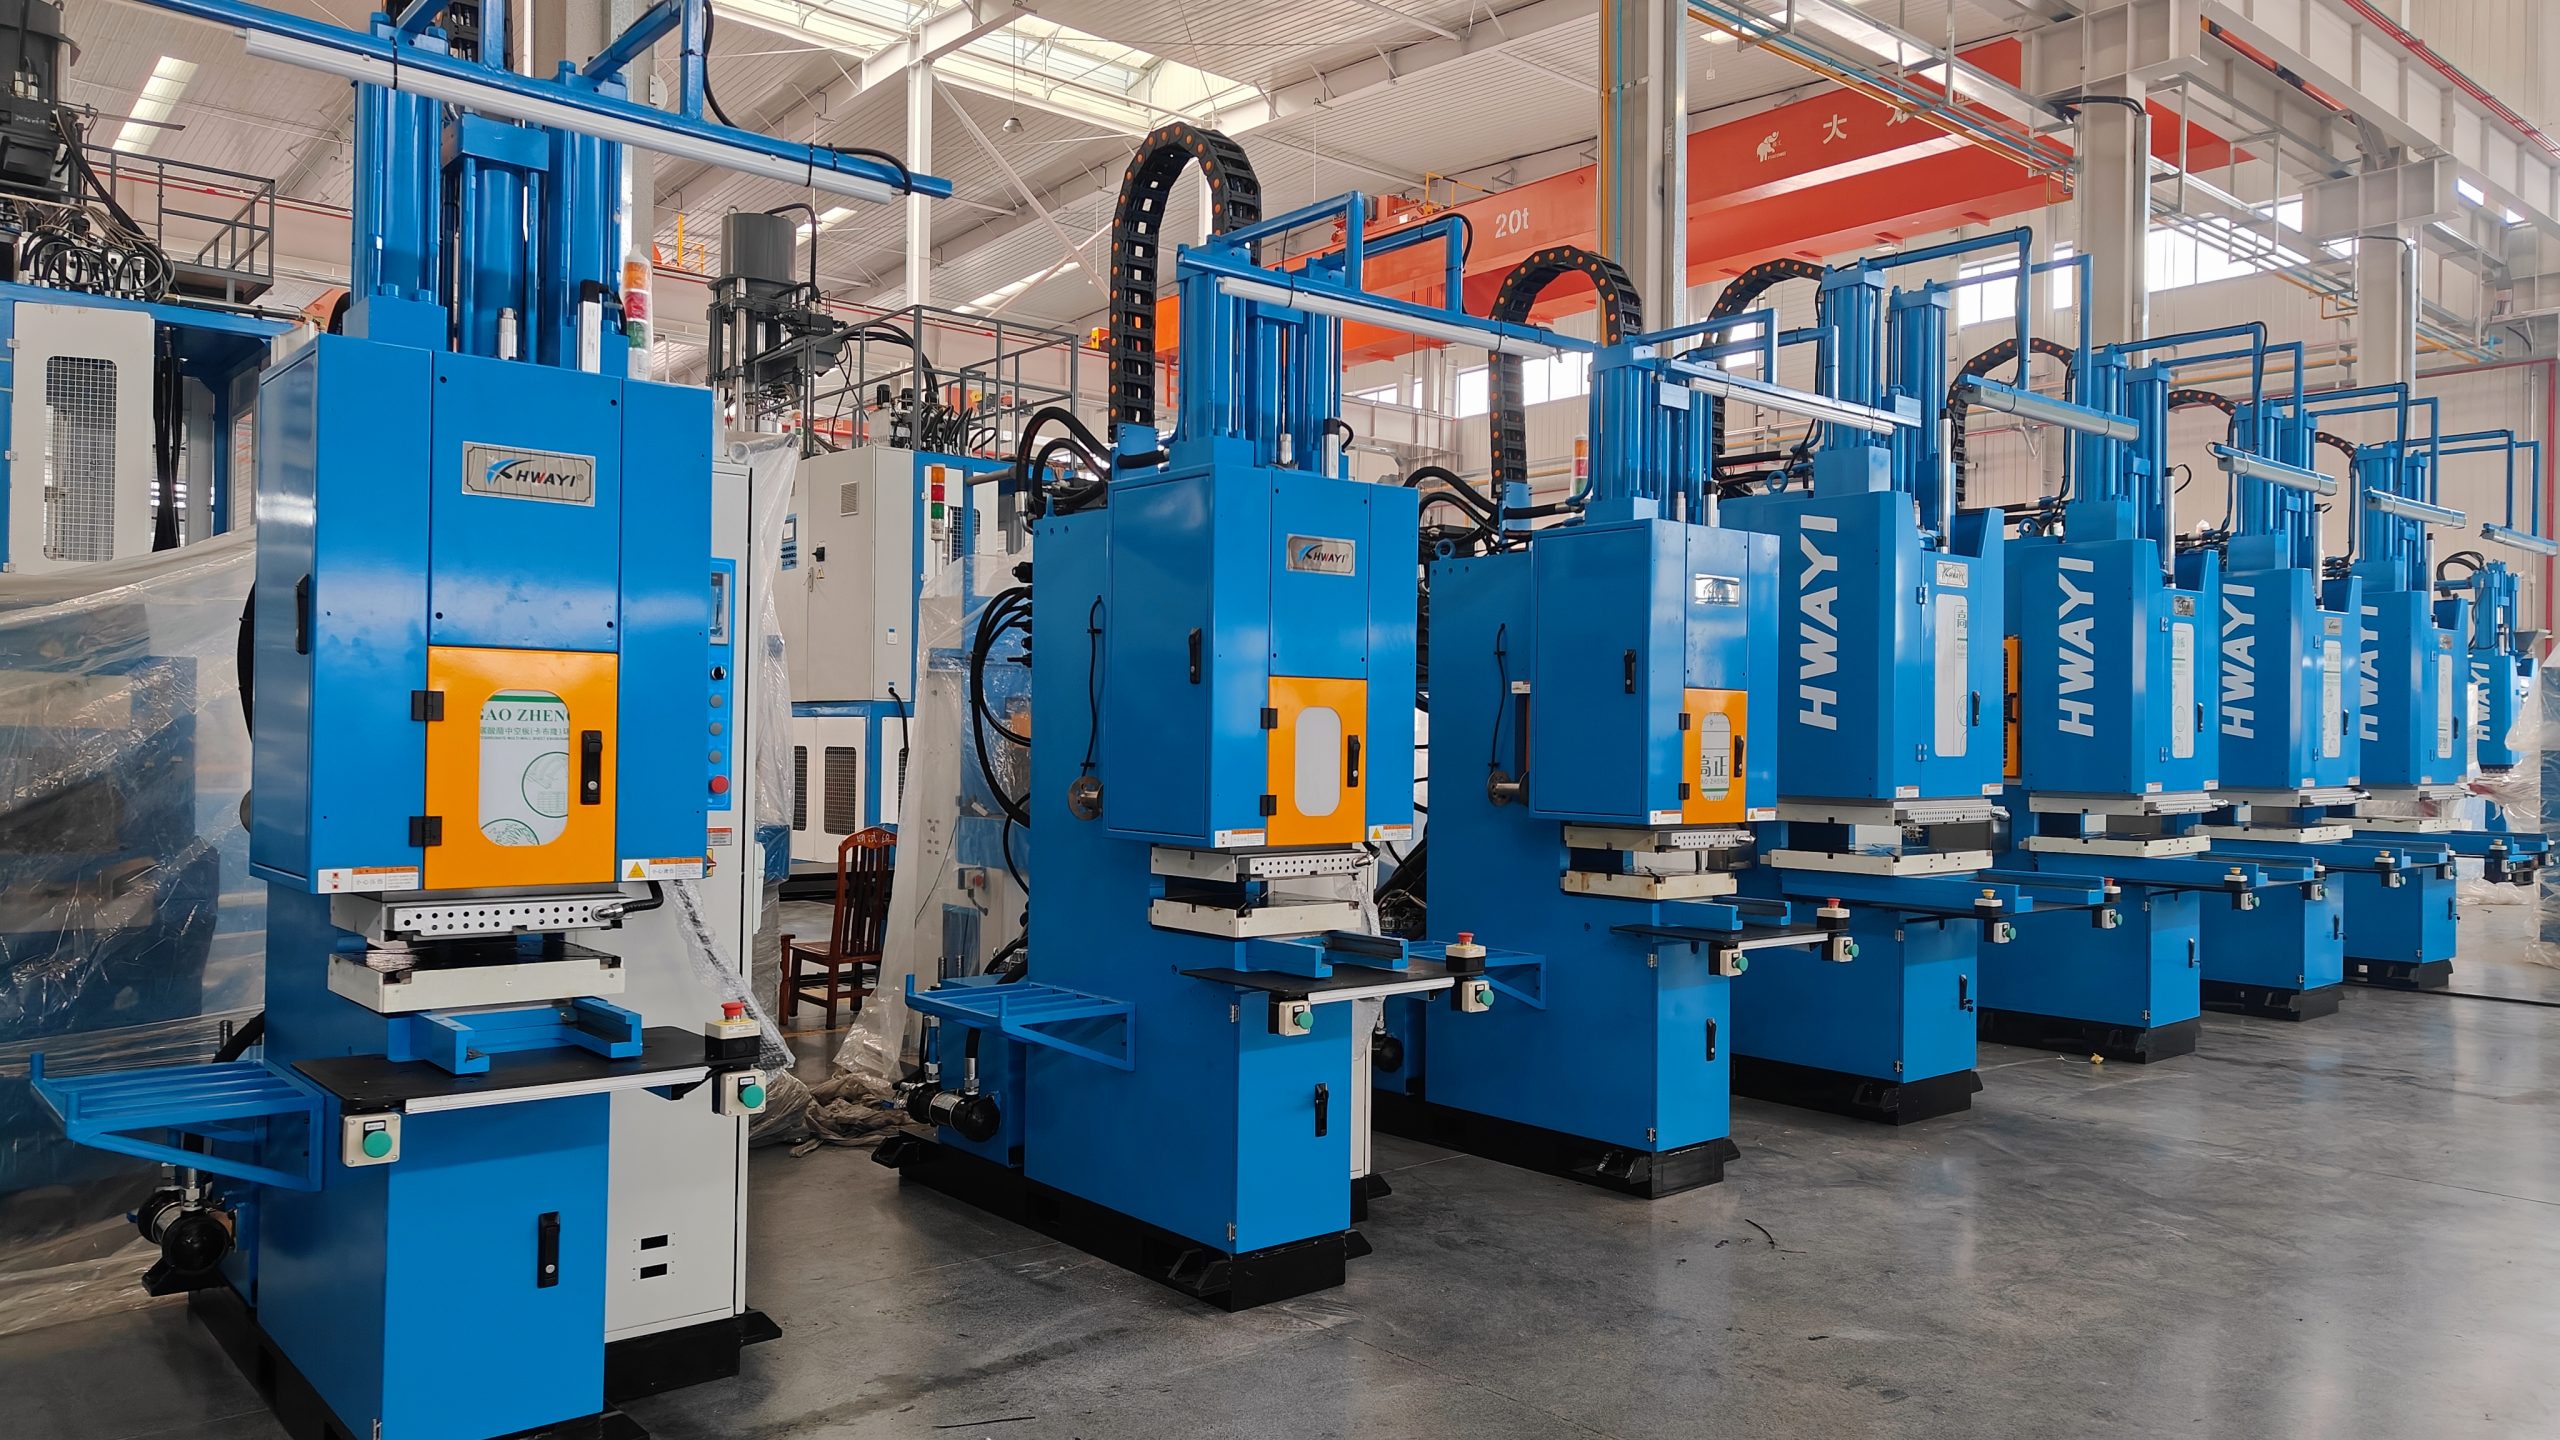
Most cycle-time pain points trace to a few concrete failures: inconsistent mold release, poor temperature control during cure, and manual strip operations. Each of those adds seconds—or minutes—per cycle. Shot size and clamping force alone don’t fix it. You need coordinated systems: a predictable injection unit, tuned cure profiles, and tooling that ejects cleanly every time. Add servo-hydraulic control and you get tighter repeatability. Simple as that—except it’s not, because tooling, machine, and operator practices must line up.
What Premium Machines Bring — Tech-Heavy, Straight
Top-tier machines deliver three game-changing features: precision temperature control, integrated mold-release sequences, and robotic or pneumatic auto-strip. Together they convert variable steps into deterministic ones. Expect shorter dwell periods, fewer manual touches, and lower scrap—especially on thin-walled parts and complex profiles where mold release is tricky. Real-world anchor: Toyota’s production discipline shows you the payoff—when a process becomes repeatable, cycle time variance collapses and throughput climbs predictably.
Practical Upgrades and Trade-offs
Upgrade paths you can actually budget for:
– Add servo-driven injection units to shrink idle strokes and tighten shot-to-shot repeatability.
– Retrofit mold heaters with zoned control to minimize cure time without overheating edges.
– Install an auto-strip system—robotic or pneumatic—matched to the part footprint to eliminate human handling delays.
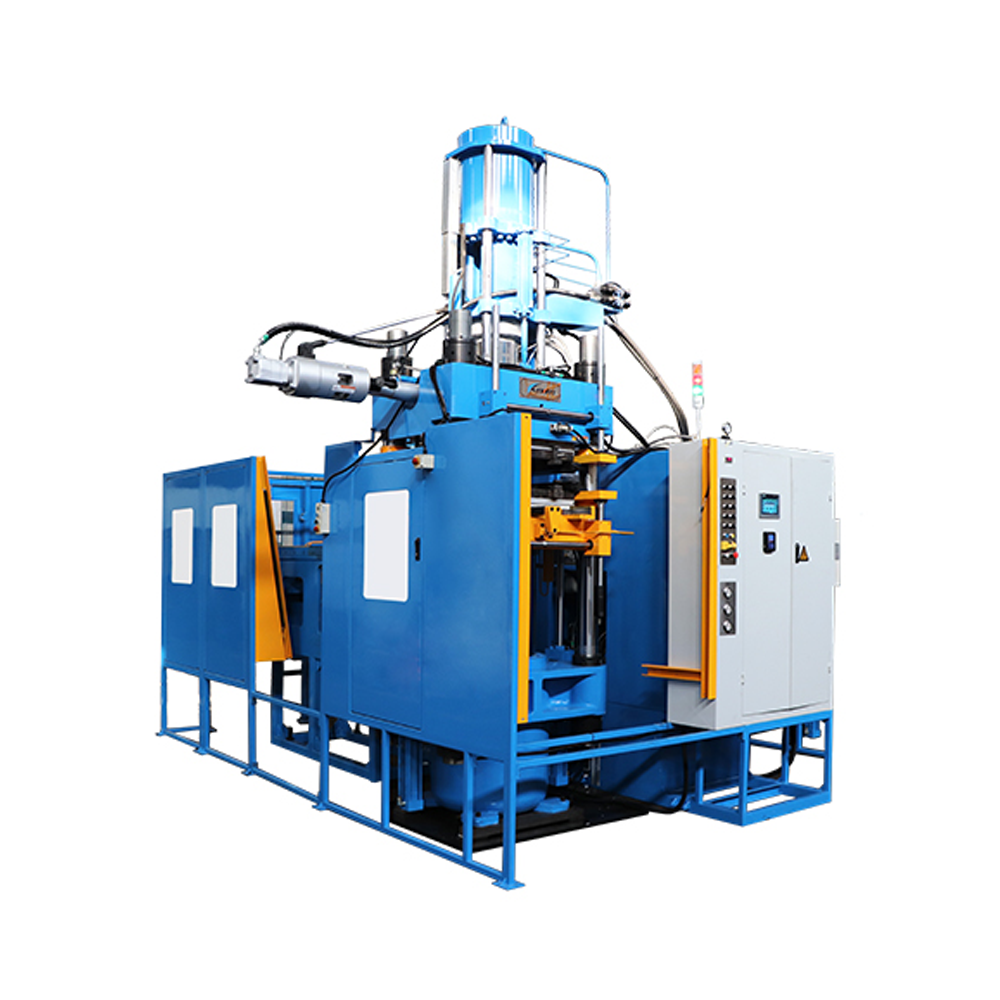
Each fix costs capital and requires setup time. But the trade-off is fewer micro-stops and lower per-part labor. You’ll need to tune cure time and demold timing carefully—rush one and you spike scrap, slow the other and you waste cycle time.
Common Mistakes Shops Make — Learn Fast
Shops often chase ultimate press speed without fixing demold dynamics. They also under-invest in tooling finish and release coatings, thinking machine upgrades alone will solve everything—wrong move. Another recurring error is treating auto-strip like a bolt-on afterthought; if cycle sequencing and ejector timing aren’t reworked, the robot just moves bad parts faster. – Keep the sequence tight: injection, controlled cure, active demold, strip. That order matters.
Alternatives and When They Fit
If capital is tight, incremental paths work: optimize mold release agents and add zoned heaters first, then add servo upgrades. For greenfield lines or high-mix shops, investing in integrated systems that combine injection control, mold temperature control, and automated stripping is smarter long-term. Also consider a flexible cobot for lower-volume auto-strip needs; it’s cheaper than a full robot and still removes manual touchpoints.
Metrics You’ll Want to Track
Measure the right stuff to verify improvements: cycle time (average and variance), first-pass yield, and mean time between manual interventions. Track cure time separately from total cycle time so you can spot gains from heating or tooling tweaks. And log ejector failures—those tell you whether demold is the real problem or just a symptom.
Advisory: Three Golden Metrics to Pick the Right Path
1) Cycle time variance: pick a system that reduces standard deviation, not just mean cycle time. Lower variance makes planning and labor sizing simpler.
2) First-pass yield after demold: a machine that shaves seconds but increases scrap is a net loss. Prioritize systems that improve yield during initial runs.
3) Mean manual interventions per shift: aim for automation that drives this metric toward zero—fewer interventions = stable operations and predictable throughput.
Final thought—real gains come from pairing tuned machines with disciplined process control. If you want hardware that behaves like a pro, look at proven platforms and thoughtful integration—especially when your line needs to behave like a clock. rubber molding machine choices matter, and the right one makes process discipline practical. HWAYI. –