



Introduction — a shop-floor morning and the numbers that nag
I was in a toolroom in Greenville one humid July morning, watching a junior tech wrestle with a part that should’ve been out the door (we’d quoted three days). The machine in question? An industrial 3d printer humming away on the bench. By noon we had three iterations, two failed supports, and a shipping delay that cost us $1,200 in expedited freight—data that bites. So here’s the real question: how do you pick and run hardware that keeps lines moving instead of stalling them?
I’ve spent over 15 years buying, selling, and fixing production gear for small manufacturers and larger contract shops. I know the ache of missed tolerance, the time-sink of post-processing, and how a single supplier decision ripples through a quarter’s P&L. This piece is written plain — southern, yes, but practical — and aims to compare real options and point you toward smarter choices. Read on for what I’ve seen go wrong, and what actually helps get parts out on time.
Next, I’ll dig into a core tech that many people assume is solved: SLA systems and where they hide trouble — then we’ll push forward into where the tech is headed.
Where SLA 3D Printers Trip Up: hidden pain points and old fixes
sla 3d printer setups look simple on paper — vat, laser, stage — but the reality on the floor is messier. I say that from hands-on runs: in March 2023 I ran a week-long validation on an RSPro-800 at our Dallas prototyping lab and saw a 12% scrap rate tied to inconsistent resin curing and warped build platform mounts. That scrap translated to a $700 consumables loss on just five builds. Direct cause? Small variables stacking up: ambient temp swings, poor support strategy, and a cured layer adhesion problem. This is not theory.
What’s the real snag?
Two big classes of pain show up. First, calibration and environmental drift: stereolithography relies on tight control of laser power, slice software parameters, and resin chemistry. A sun-facing window or an HVAC cycle can shift cure behavior. Second, post-processing and support structures: parts that look fine on the build plate can tear during support removal, especially on thin-walled geometries. I often see shops default to heavier supports — that lowers build failure but hikes finish time and manual labor.
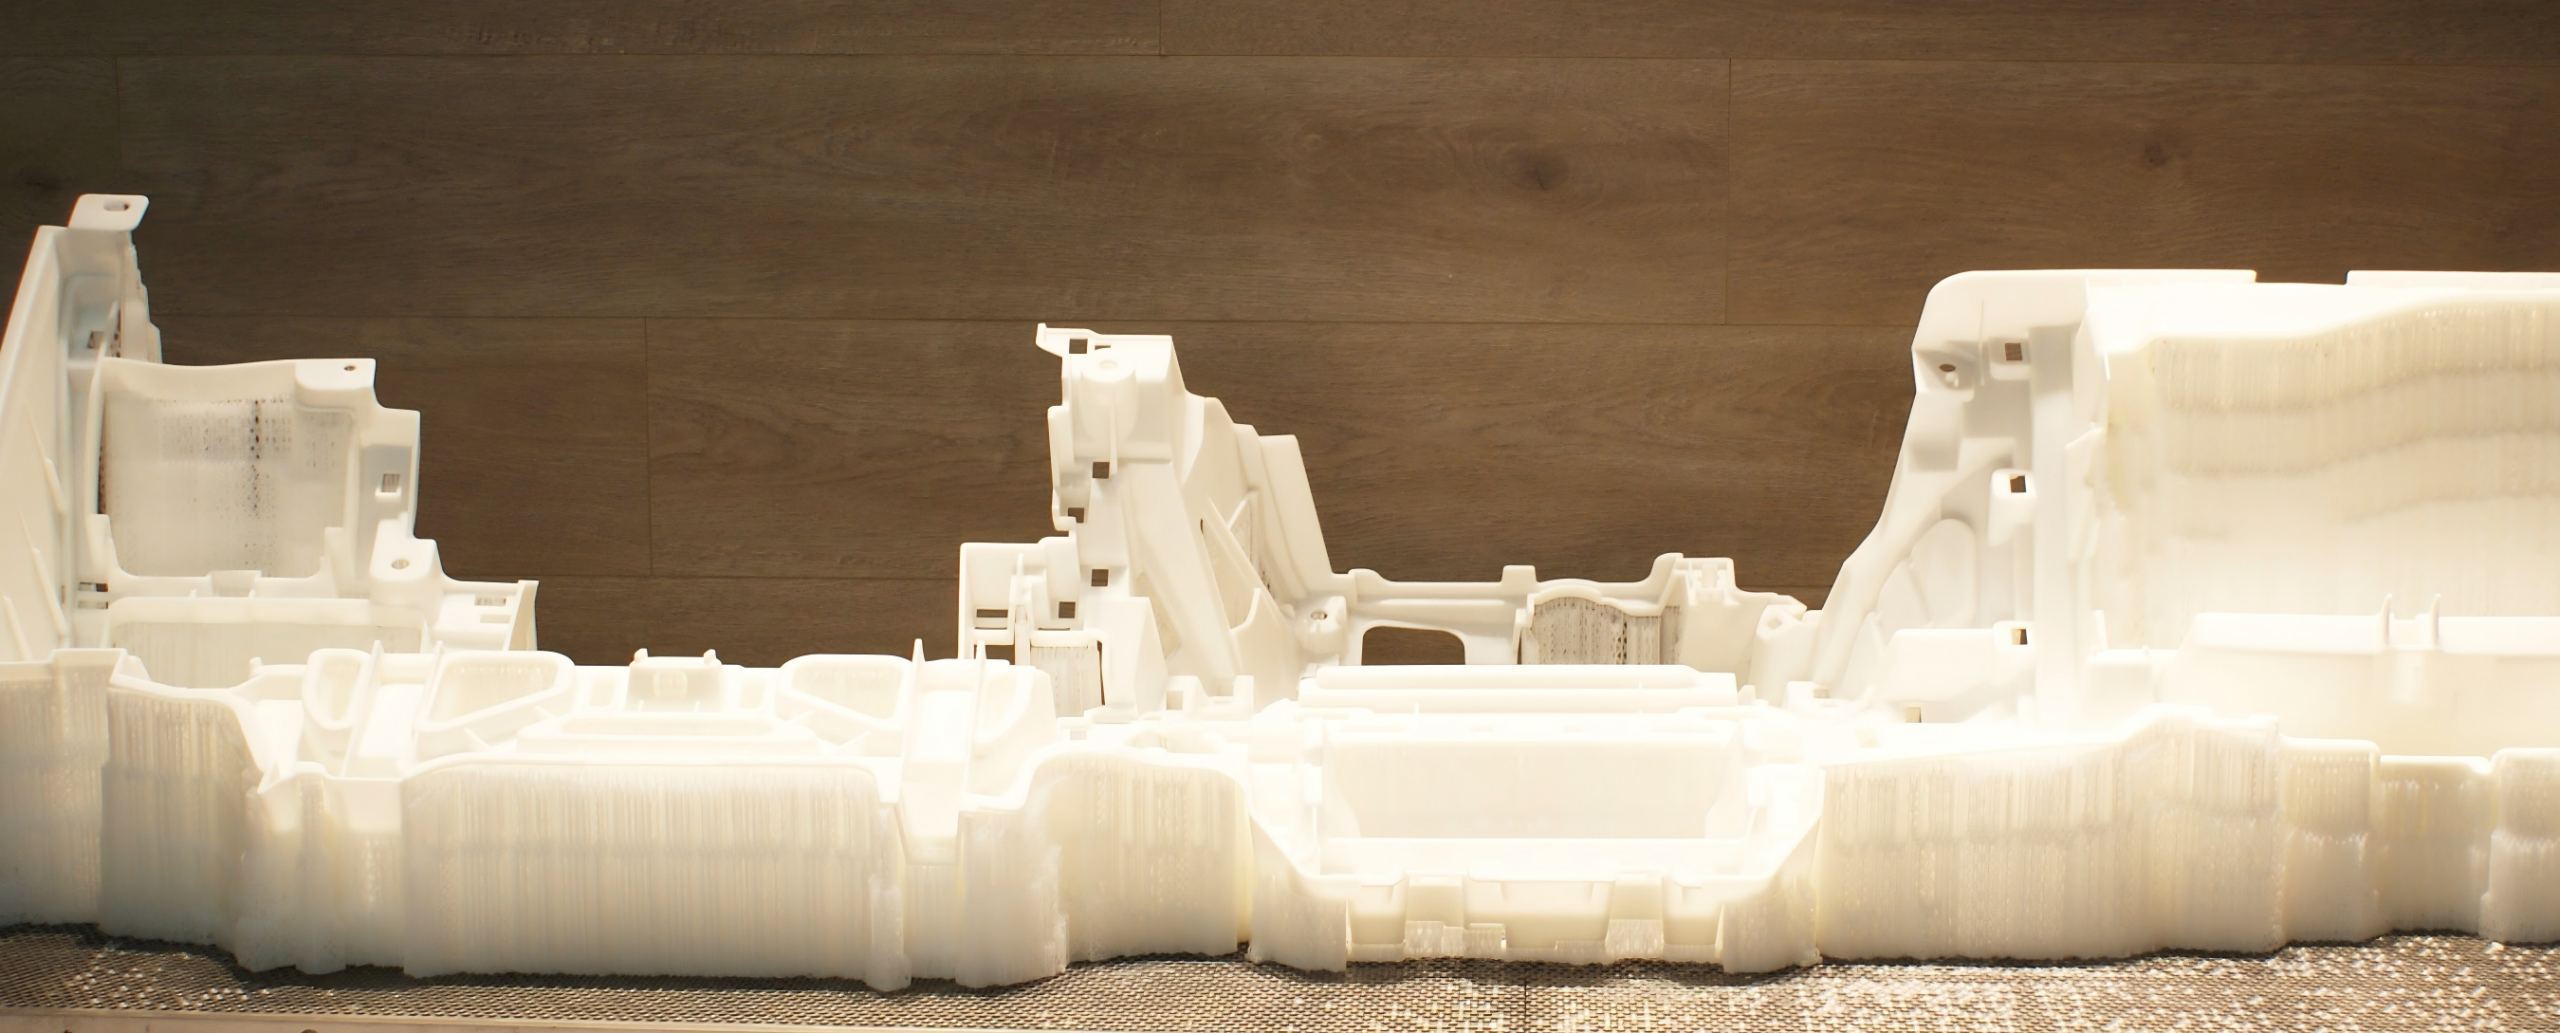
Look, I’m not saying SLA is a bad choice. I prefer SLA for fine detail and smooth surfaces (jewelry, dental fixtures, small aerospace jigs). But if you don’t account for resin batch variance, vat wear, and the need for robust fixturing, you end up firefighting. Add in industry terms: resin curing, build platform alignment, support structures, and you get a realistic checklist of failure points. Practical tip: keep a dated log of resin lot numbers, ambient readings, and laser power checks — I guarantee it saves a week of troubleshooting down the line.
Forward-Looking: case examples and practical metrics for choosing new machines
Now let’s look forward. I ran comparative trials last fall (October 2024) comparing two SLA lines and one DLP backup for short-run production. The winner wasn’t the fanciest controller; it was the machine with predictable maintenance intervals and easy vat swaps. If you’re evaluating options, consider this case: switching to a model with a modular vat cut our cleaning time by 35% and reduced downtime by two maintenance sessions per quarter — measurable cash saved.
Real-world Impact
One concrete example: a contract shop in Chattanooga swapped to a mid-range SLA unit with an automated peeling mechanism and pre-set resin profiles. Within sixty days they saw a 20% throughput gain on dental models and a 40% drop in operator rework. The changes were straightforward — updated slice profiles, stricter QC on incoming resins, and a little training. These are the sort of returns that make a difference in monthly margins.
As for technology principles: look for machines that ease three things — predictable curing (accurate laser or projector calibration), modular consumables (quick vat, exchangeable build platforms), and clear service pathways (replaceable power converters, documented firmware updates). Also, monitor your edge processes: a small investment in a dedicated post-cure station and a repeatable wash schedule often yields better consistency than chasing firmware settings. — this is practical, not speculative.
How to evaluate your next industrial 3D printer — three key metrics
I’ll leave you with three concrete metrics I use when advising procurement managers:
1) Mean Time Between Maintenance (MTBM) measured in operational hours. Ask vendors for field MTBM numbers and validate with user references from similar production mixes (e.g., dental runs vs. small aerospace jigs).
2) Effective Throughput per Shift. Don’t rely on stated print speed. Run or request a representative build pack: actual mixed-batch throughput over an eight-hour shift, including post-processing and operator touch time.
3) Consumable Variance Cost. Track the real cost per usable part, factoring in resin scrap, vat life, and support waste. In my experience, two printers with similar capex can have 30–50% different part costs once consumables and labor are counted.
If you score vendors on those three metrics, you’ll avoid the shiny-promise syndrome and pick systems that fit your workflows. For hands-on support and reliable hardware options, I often point peers toward established providers who publish service data and field references — for example, UnionTech.
I write this from years in the trenches — over 15 years at the buying desk and on the shop floor — and I stand by these practical measures. Make decisions that reduce surprises, and you’ll keep parts moving and customers smiling. UnionTech