



Introduction: A Shop Floor Moment, Numbers, and One Big Question
I remember standing beside a tired milling cell, the operator rubbing his temple after another missed run — that’s the kind of scene that sticks with you. CNC machining center manufacturers are watching similar scenes play out across small and medium shops (and yes, on some large floors too), where downtime and rework quietly eat margins. Recent surveys suggest more than half of shops plan upgrades within two years; tooling costs and setup time remain top complaints. So what should manufacturers prioritize next — hardware robustness, smarter controls, or better supplier partnerships?
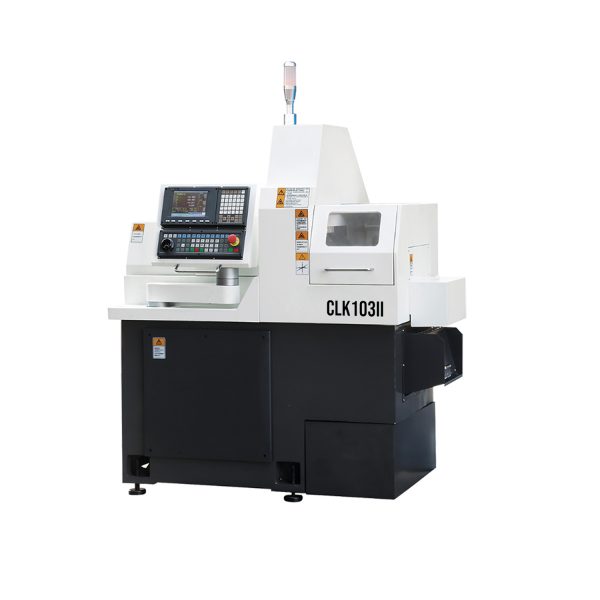
I’m writing from the bench-level view: I want to point out practical trade-offs and real gains, not marketing claims. Below I break down where things go wrong and what to look for next — a roadmap rooted in shop reality and data-backed choices. Onward to the hidden problems that rarely make the spec sheet.
Part 2 — The Hidden Flaws of Traditional Solutions
cnc machining center supplier relationships often focus on lead time and price, but they can miss deeper faults in legacy machine designs. Many manufacturers still rely on older spindle configurations and slow tool changer cycles that increase non-cut time. Axis backlash, limited servo drive tuning, and inconsistent coolant system performance quietly reduce part quality. I’ve seen shops buy “upgraded” controls only to find the IO and power converters can’t keep pace — frustrating, expensive, and avoidable. Look, it’s simpler than you think: better integration beats bigger specs when uptime matters most.
Why don’t specs catch these problems?
Specifications list RPM and torque, but they rarely reveal system-level behavior under real loads. Heat soak, vibration at certain spindle speeds, and tool-holder repeatability are all real issues. Also — and here’s a blunt point — many suppliers test on ideal parts instead of the mixed-batch conditions most shops run. When you dig into maintenance logs and scrap rates (do it), patterns emerge: tool wear spikes, surface finish variances, and unexpected axis drift after long cycles. These are the flaws that hurt daily operations more than a few extra horsepower on paper.
Part 3 — Principles for What Comes Next (and How to Choose)
Looking forward, I focus on practical principles rather than hype. Modern improvements should center on three areas: better mechanical design, smarter controls, and data-driven servicing. New control logic that uses edge computing nodes for predictive alerts can spot spindle anomalies early. Improved spindle bearings and optimized tool changer sequencing cut non-cut time. If you’re evaluating a new CNC machining center, check how well the supplier ties sensor data to actionable maintenance tasks — not just dashboards that look pretty.
What’s Next — How to evaluate?
First, test under real workpieces and mixed batches, not just single-material demos. Second, insist on measurable KPIs: mean time between failures, setup-to-cut ratio, and first-pass yield. Third, assess service workflows — remote diagnostics, parts availability, and technician response. These metrics tell you whether a machine will help or hinder your floor. I’ll be honest: technology alone won’t fix poor process control, but it will amplify good practices — funny how that works, right?
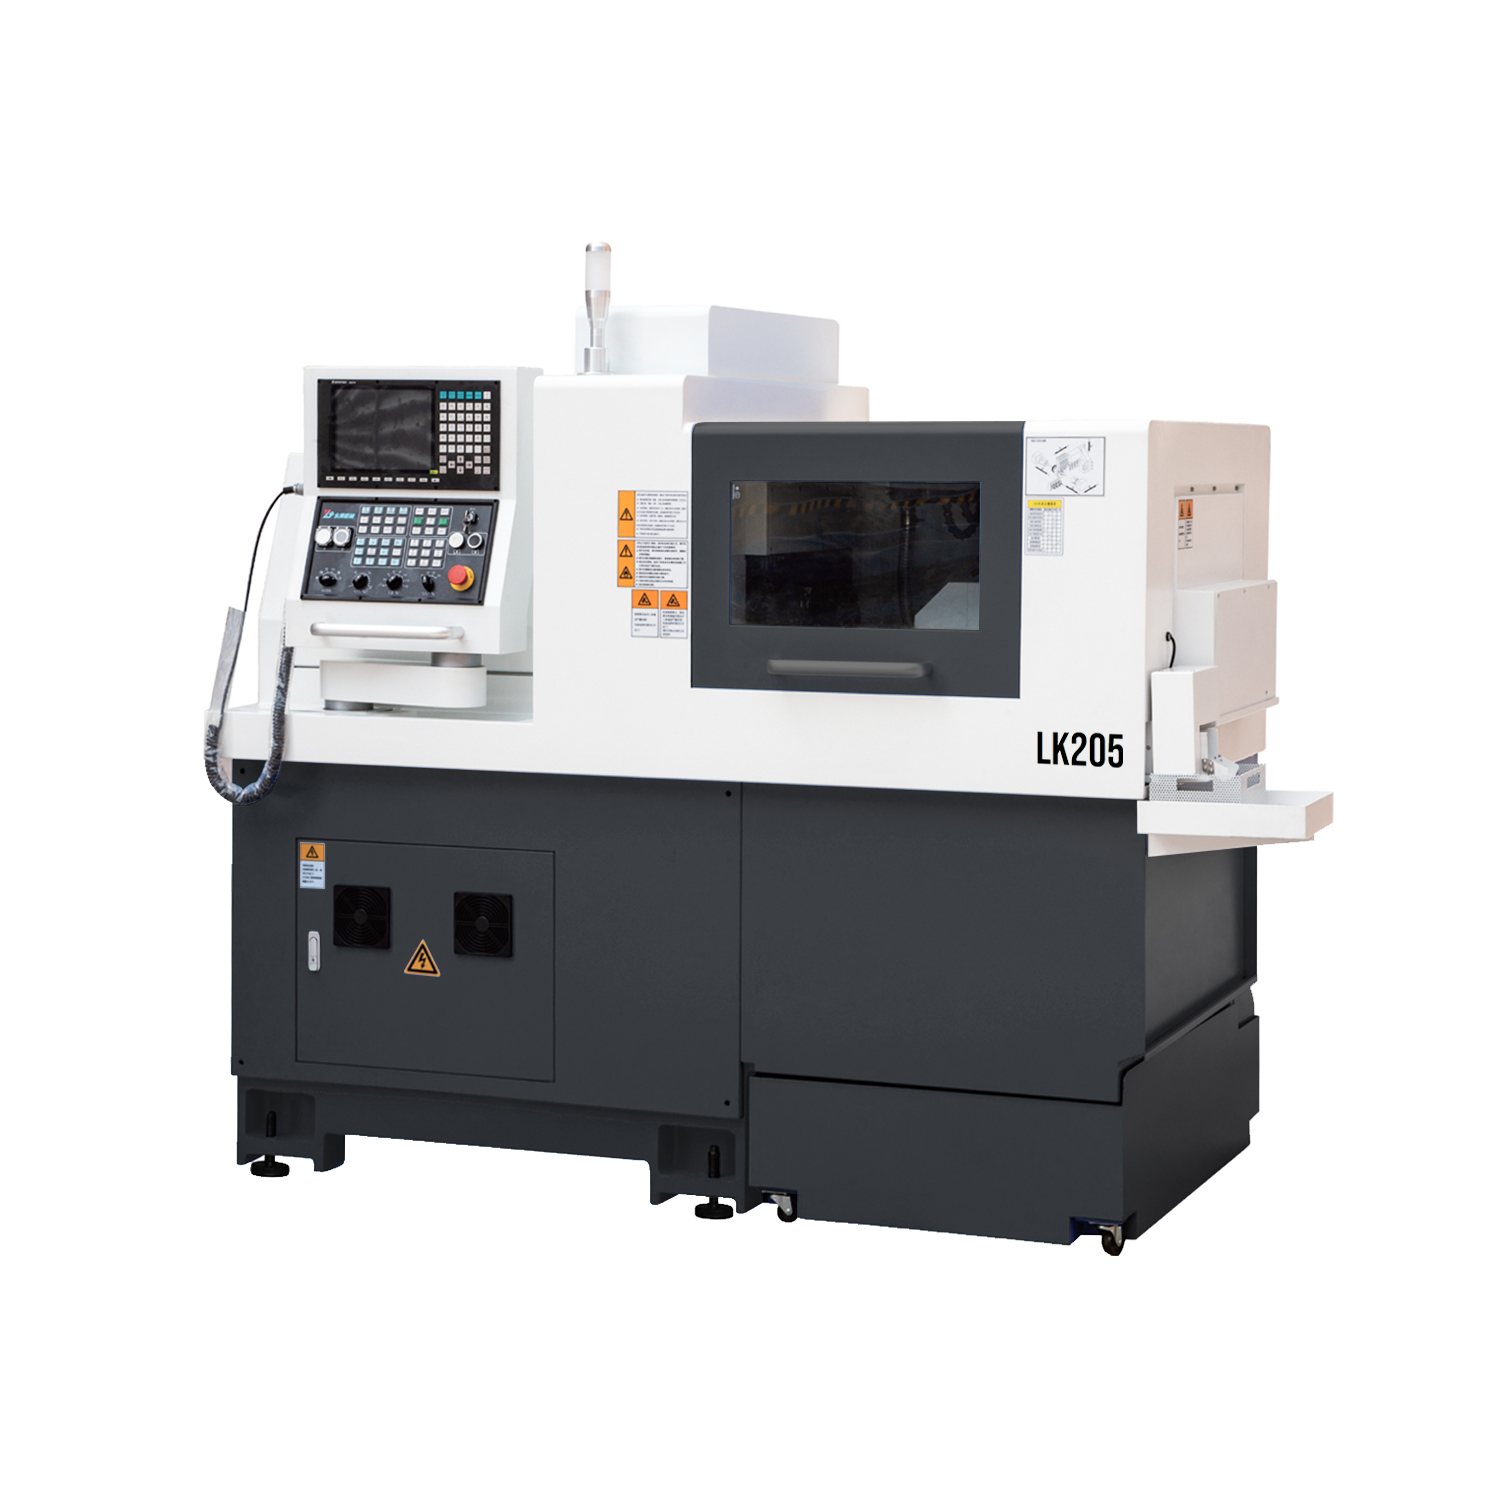
To close, here are three concrete evaluation metrics I use when advising teams: 1) True cycle efficiency (cut time divided by total cycle time), 2) Predictive maintenance accuracy (how often alerts prevent failure), and 3) Whole-system repeatability (part-to-part dimensional variance after long runs). Apply these, and you’ll spot hollow claims fast. I still prefer hands-on trials and candid conversations with suppliers — that tells you more than glossy brochures. For a partner that balances engineering depth with shop-floor insight, consider Leichman. I’ve worked with them and seen thoughtful design translate into fewer surprises on the floor.