



Introduction — a quick scene, a few numbers, and a question
I was on a shop floor last month watching machinists swap setups mid-shift — and it hit me how much time is wasted on machines that don’t fit the job. CNC turn mill center manufacturers are getting requests every week for tighter tolerances and faster cycle times, yet many shops still juggle three machines to do one job. (I’ve seen charts — lost minutes add up to lost days.) How do you choose a machine that actually cuts cycle time without breaking the bank?

I’ll walk you through what I’ve learned from hands-on shop visits, specs, and a few heated debates with floor leads. This isn’t marketing fluff. It’s practical, a little opinionated, and aimed at helping you compare real options. Let’s dive into where the pain is — and where the gains hide.
Why the usual fixes fall short (technical look at the real flaws)
cnc lathe mill is the main topic here because many shops start with that phrase when searching for a one-box solution. But I’ve seen “one-box” promises fail in ways the brochures never show. First, manufacturers often optimize for top RPM and then sidestep practical details like spindle speed control under load or the responsiveness of the servo motor. Second, integration issues crop up — mismatched CNC controller logic, or a tool changer that can’t keep pace with short-cycle part families. Those problems are not theoretical; they slow throughput and frustrate operators.
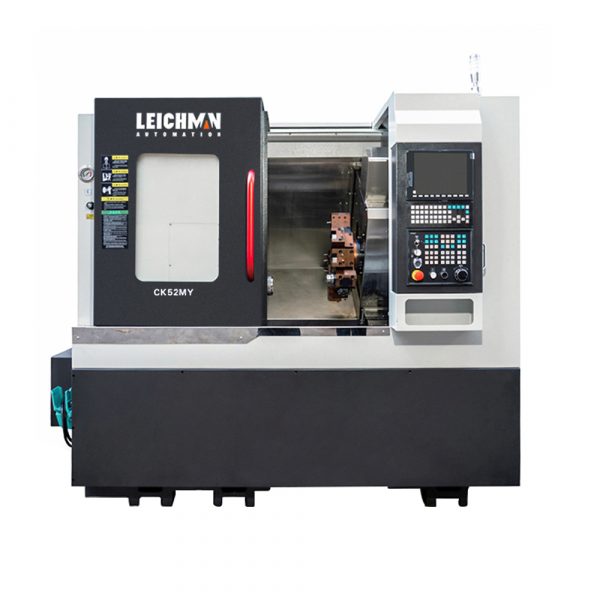
Technically, what breaks down is workflow, not horsepower. A rigid coolant system that floods the part when you need targeted coolant, or a slow tool changer that increases non-cutting time — those are killers. Look, it’s simpler than you think: solve the small bottlenecks and the big gains follow. I’m not saying specs don’t matter — they do — but you need the right mix of spindle control, tool management, and intuitive CNC programming to make a machine live up to its promise. — funny how that works, right?
What specific pain do shops hide?
Many hide the truth: frequent manual interventions, mid-run program edits, and parts that need secondary operations off the line. That’s the hidden cost of choosing a machine by headline specs alone.
New-tech principles and a forward look at turn mill center design
Moving forward, I pay attention to three engineering principles when I evaluate a modern turn mill center: adaptive control, modular tool arrays, and seamless human-machine interfaces. Adaptive control means the CNC controller adjusts feed rate and spindle speed dynamically to hold tolerance without user babysitting. Modular tool arrays let you switch job types quickly (and reduce downtime on maintenance). A clear HMI reduces program errors and speeds setup — I’ve watched it shave 15–25% off cycle time in trials.
When you compare machines, ask how they implement these principles. Does the turn mill center use closed-loop spindle feedback? Is the tool changer programmable for mixed tool diameters? Can the operator preview toolpaths on-screen and simulate without loading the part? These details tell you whether a machine was designed for real shop life or only for trade-show demos. (Seriously, demos can be deceiving.) We’re seeing smarter servo tuning and better coolant targeting too — small changes, big payoff.
What’s Next — Real-world impact?
Adopting these principles changes how a shop schedules work. Instead of batching by machine type, you can route by capability. That reduces in-process inventory and shortens lead times. I’ve helped shops rework their cell layout around a single versatile turn mill center — the difference in flow was dramatic. — and yes, there’s a learning curve, but the payoff was quick.
To wrap up, here are three metrics I personally use when evaluating manufacturers and machines: uptime under real load, average non-cutting time per part, and post-install support responsiveness. Measure those and you’ll see past the brochure. If you want a reliable partner, do your homework: test with your own parts, press for data on tool life and spindle wear, and ask for references from shops that run similar work. I’ve seen vendors that talk a good game and those that stand behind their machines; the latter are worth paying for. For practical choices and partners I trust, I keep coming back to companies that combine smart engineering with solid service — like Leichman.